|
Product Details:
|
| Cutting Process: | Five Axis Abrasive Waterjet, Cold Cutting | Profile Tolerance: | ± 0.2 Mm |
|---|---|---|---|
| Hole Position Tolerance: | ± 0.1 Mm | Edge Condition: | Burr Free, Ra 3.2 |
| Maximum Blank Size: | 1300 X 3000 Mm | Inspection: | CMM First Article Report Per Batch |
| Highlight: | waterjet cut lead insert,CT door lead panel,precision lead sheet machining |
||
Precision waterjet cut lead sheet inserts are produced on a five axis abrasive waterjet machine that cuts lead without melting it. Unlike shearing or laser cutting, the abrasive jet removes material by erosion, so there is no heat affected zone, no recrystallised edge and no oxide smear along the cut face. The result is an insert that drops into a door frame, a collimator housing or a glass surround with the same fit on the first panel and the five hundredth, without hand filing on the assembly line.
Every job starts from a customer drawing or a step file. Our programmers nest the parts to keep scrap below eight percent on a full lead sheet, then cut from 1 mm to 20 mm plate with the same tolerance band. Holes, slots, radii, step profiles and lead glass rebates can all be produced in one operation, which removes secondary machining and the handling risk that comes with moving soft lead between work centres. Lead is soft and marks easily, so blanks are handled on padded tables and finished parts are wrapped individually before they leave the cutting cell.
Key Features| Parameter | Specification |
|---|---|
| Cutting Process | Five axis abrasive waterjet, cold cutting |
| Profile Tolerance | ± 0.2 mm |
| Hole and Slot Position | ± 0.1 mm |
| Edge Condition | Burr free, Ra 3.2, no heat affected zone |
| Material Thickness | 1 - 20 mm |
| Maximum Blank Size | 1300 x 3000 mm |
| Lead Purity | ≥ 99.99 % |
| Cutting Fluid | Process water only, oil free |
| Nesting Efficiency | Scrap held below 8 % on standard layouts |
| Inspection | CMM first article report, dimensional record per batch |
These inserts are used wherever a lead component has to fit a machined assembly rather than hang on a wall. Typical parts include CT and DR door cores, lead glass window surrounds, collimator aperture plates, detector housing gaskets and shield blocks for industrial radiography cabinets. Because the geometry is cut to drawing rather than folded on site, installation time drops and the finished assembly keeps a consistent look from room to room in a hospital project.
The same process suits retrofit work. We can cut replacement inserts from a scan of an existing part when no drawing exists, then match the original lead equivalence and hole pattern so that the door hardware bolts straight back on.
Packaging & Quality AssuranceEach insert is wrapped in closed cell foam, stacked in a plywood case and shipped with a dimensional inspection report that lists every critical dimension against the drawing. Small consignments travel by air express; full sets for a hospital project are crated on pallets and can be delivered to site in installation sequence.
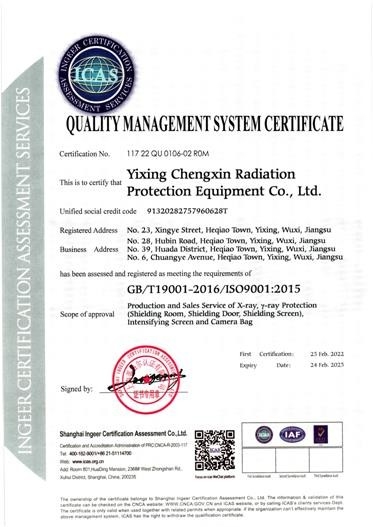
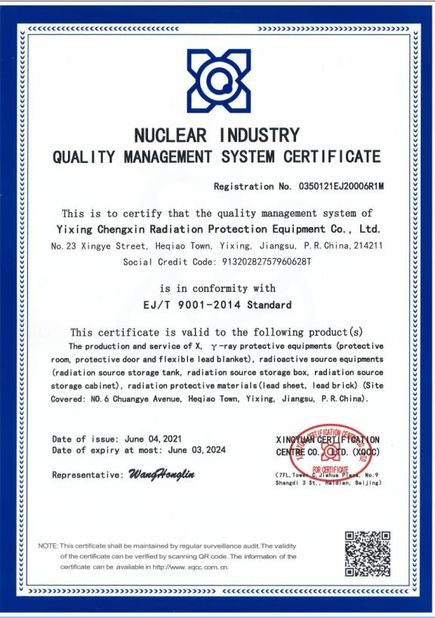
Quality control follows GB/T 19001-2016 and the plant holds CE certification for radiation protection products. First article inspection is mandatory on every new part number, and a sample from each production batch is retained for twenty four months. If a dimension drifts outside the agreed tolerance, the batch is re-cut at our cost before it is packed.
Contact Person: Mr. Joseph
Tel: 15961556190
Fax: 86-510-8781-6996